How to Cut and Join Strut Channel on Site
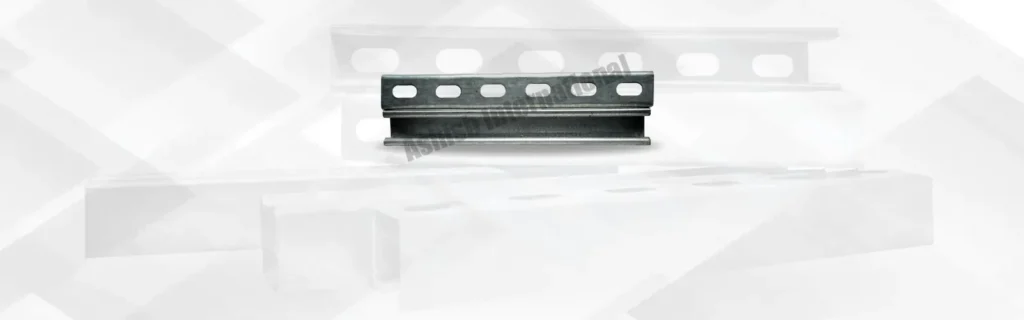
To cut and join strut channel on site, you measure and mark the channel, cut it square with a chop saw, bandsaw, or angle grinder, deburr the sharp edges, and treat the bare cut with zinc spray to stop rust. You then join two lengths by overlapping them or bolting a splice plate across the joint, using standard channel nuts and bolts. Because every strut channel shares the same 41 mm width, fittings and splices fit any length, which is what makes on-site fabrication so quick. Two things catch people out: leaving cut edges bare — galvanised steel rusts from an untreated cut — and cutting out of square, which weakens a joint. Ashish International, with 25+ years of manufacturing experience, supplies strut channel and matched fittings built for clean cutting and strong splicing. This guide walks through cutting, joining, and finishing channel safely. Should You Cut On Site or Order It Cut? Before reaching for a saw, it is worth knowing when site-cutting is the right call and when factory-cut channel wins. The table below weighs the two. Factor Site-cut channel Factory-cut / fabricated Speed for one-offs Fast, done on the spot Needs ordering ahead Cut-edge protection Manual zinc touch-up needed Coated or re-galvanised properly Consistency at volume Varies by operator Identical every piece Complex assemblies Harder to get right Built and checked in-house Best for Adjustments, small runs Repeat orders, exact specs The sharpest difference is corrosion protection: a factory can re-galvanise a cut part fully, while a site cut relies on a sprayed touch-up that never quite matches the original coating. For large or repeat orders, fabricated steel products cut and finished in a plant save both time and long-term rust risk. Site-cutting suits adjustments and small runs; factory work suits volume and exact specs. The Right Way to Cut a Length When the job calls for cutting on site, a clean square cut is the base of every strong joint. Follow the steps in order: Measure and mark — mark the cut line clearly, allowing for any overlap at joints. Clamp it down — secure the channel so it cannot shift mid-cut. Cut square — use a chop saw or bandsaw for the cleanest edge, or an angle grinder where a saw cannot reach. Deburr the edge — file or grind off the sharp burr, which also removes the injury risk. Treat the cut — apply cold-galvanising zinc spray to the bare edge to restore corrosion protection. An out-of-square cut is the one that most often fails later, because it leaves a gap at the joint that loosens under load. A straight, deburred, treated cut turns a raw length into a ready-to-join section. Keep These Tools on the Trolley Cutting channel needs no specialist kit, but a few tools make the job faster, safer, and cleaner: a chop saw or portable bandsaw for square repeat cuts, an angle grinder for tight spots, a file or deburring tool for the sharp edge, cold-galvanising zinc spray for the bare cut, and tape, square, and marker for an accurate line. A cordless bandsaw has become the site favourite because it cuts square with far less spark and noise than a grinder. Keep the deburring tool and zinc spray beside the saw and the two most-skipped finishing steps stop getting missed. Joining Two Sections That Actually Hold With lengths cut, joining them is straightforward, and the method depends on the load the joint must carry. The simplest is an overlap: slide two channels together over a short length and bolt them with channel nuts, which suits light runs. For a stronger, in-line joint, a strut channel splice uses a splice plate or connector across the join, bolted through both channels to transfer load smoothly across the gap. Heavier runs often step up to a back-to-back strut channel or a deeper section rather than relying on a single spliced length. Whichever method you use, the 41 mm width means your spring channel nuts, threaded rod, and beam clamps fit the same across every joint. A joint is only as strong as its fixings, so rated hardware matched to the channel keeps a spliced run safe. The Two Steps Crews Rush — and Shouldn’t Two finishing steps are quietly the most important, and both are the ones crews cut short: Deburr and wear PPE — every cut leaves a razor-sharp burr, and cutting throws sparks and metal dust, so file each edge and use gloves and eye protection. A filed edge is safer to handle and makes a cleaner joint. Re-coat every cut — cutting galvanised channel exposes bare steel that rusts from the edge if left untreated, so apply zinc-rich cold-galvanising spray, especially outdoors or in wet MEP support structures. For coastal, rooftop, or wet sites this touch-up matters even more, which is why many specifiers order pre-cut pre-galvanised slotted channel or stainless steel channel to reduce field cuts altogether. Treat every cut edge and it becomes the cheapest insurance against a support rusting years early. Save the Field Work — Order It Cut to Spec Every cut made on site is one more edge to deburr, coat, and get square — and at volume that adds up fast. This is where ordering pre-cut pays off, and where three decades of manufacturing help: Ashish International cuts, splices, and re-galvanises to spec across three units and 60,000 square feet, at 350 tonnes a month under in-house quality control, so channel arrives ready to install with edges properly protected. Contractors, stockists, and sourcing companies across the UK, Europe, the Middle-East, Australia, and Africa order this way to cut site labour, and several have relied on us for over 20 years, some under NDA for their own designs. We manufacture to international dimensions with a consistent 41 mm width, and for brands and MNCs we run the full service as white-label — your spec, your branding, FITSTRUTS® where a stock line fits. For custom-cut channel, splice fittings, or a white-label discussion, call +91-99888-54380
Strut Channel Sizes in India | Dimensions & Weights
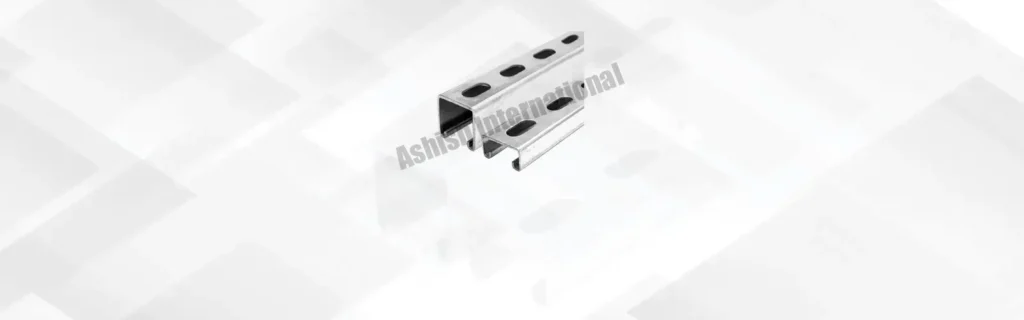
Strut channel sizes in India are built around a standard 41 mm width, with the height, steel gauge, and finish changing to suit the load and environment. The most common size is 41×41 mm (full height), followed by 41×21 mm (half height), plus deeper profiles like 41×62 mm and 41×82 mm for heavy runs. A 41×41 mm channel in 2.5 mm steel weighs about 2.8 kg per metre, while lighter 1.5 mm versions run closer to 1.5–2.1 kg per metre. Channel is sold in standard 3-metre and 6-metre lengths, in slotted or plain form, and in pre-galvanised, hot dip galvanised, or stainless finishes. You choose a size by matching width, height, gauge, and finish to your support job. Ashish International, drawing on 25+ years of production, manufactures the full range of strut channel sizes to international dimensions. This guide lists the standard sizes, their weights, and how to pick the right one. The Four Things Every Size Spec Tells You Read from left to right, a size spec answers four questions at once. Learn these and no supplier’s list is a mystery: Width — almost always 41 mm, because that is what keeps standard nuts, bolts, and fittings compatible worldwide. Height — the number that changes most; taller means more load, shorter means lighter and space-saving. Gauge — the steel thickness, which quietly decides both strength and price for the same size. Finish — galvanised or stainless, matched to indoor, outdoor, or hygienic use. Buyers most often forget to ask about gauge, yet two channels of the same size can differ sharply in strength and cost because of it. Once width, height, and gauge read together, choosing from a range becomes quick. What the Size Numbers Mean in Practice The two figures in a size like 41×41 are simply width and height in millimetres. The width holds at 41 mm across nearly every profile, which is exactly why a channel nut, bolt, or bracket slots into any of them — it is the figure that keeps the whole system interchangeable. The height is what shifts the job: a taller 41×41 profile acts like a deeper beam and carries more load, while a shallower 41×21 profile saves weight and space where the load is light. The most requested single figure — the 41×21 channel weight per metre — sits around 1.3–2.1 kg depending on gauge, handy for costing a light run at volume. Read width and height together and a size maps to a real support rather than a guess. Standard Sizes and Weights, Side by Side With the basics clear, the chart below covers most of what buyers need, since the Indian market follows the same core profiles as global brands. It sets out the standard GI channel sizes, typical weight per metre, and where each fits. Size (W × H) Typical gauge Weight per metre Common use 41 × 21 mm 1.5–2.5 mm ~1.3–2.1 kg Light cable and conduit runs 41 × 41 mm 1.5–2.5 mm ~1.5–2.8 kg General MEP support, the standard 41 × 62 mm 2.0–2.5 mm ~3.5–4.5 kg Medium-heavy pipe and duct runs 41 × 82 mm 2.5 mm ~5 kg+ Heavy racks and long spans Back-to-back 2.5 mm ~5.6 kg+ Very heavy or long unsupported runs Weight rises with both height and gauge, so a heavier number on the spec sheet usually signals more load capacity. Read the size chart first and shortlisting the right channel comes before finish or length. Don’t Forget Finish and Length A size alone is not an orderable part — finish and length complete it. Finishes run from pre-galvanised for dry indoor use, to hot dip galvanised iron channel for outdoor and corrosive sites, to stainless steel in SS304 or SS316 for food, pharma, and coastal duty. Standard lengths are 3 metres and 6 metres, with custom cuts on request, and a common Indian slot detail is a 12 mm × 24 mm opening sized for standard threaded rod. Pair finish and length with size and a dimension becomes a part you can actually order. Choosing the Right Size, Step by Step With the range and specs understood, selecting a size is a short, ordered decision. Work through it in this order: Start with the load — heavier weight needs a taller profile or thicker gauge. Check the span — long unsupported runs need 41×62, 41×82, or a back-to-back strut channel. Measure the space — tight ceilings suit the low-profile 41×21. Match the finish to the environment — indoor, outdoor, or hygienic. Confirm the fittings — the 41 mm width keeps spring channel nuts and threaded rod compatible across sizes. Get the load right at step one and it drives the whole choice, because an undersized channel is the most common and costly sizing error. Match size to the job rather than to what is on the shelf, and a support stays both safe and economical — the same logic behind well-planned MEP support structures. The Full Size Range From One Maker Sourcing a mixed size list from one supplier saves the headache of matching parts from several — and a manufacturer with real range makes that possible. Ashish International produces every profile from 41×21 to back-to-back across three units and 60,000 square feet, at 350 tonnes a month under in-house quality control, all to consistent international dimensions. Our channel already sits on major Indian B2B marketplaces, and we ship to sourcing companies, stockists, and B2B contractors across Europe, the UK, USA, Australia, the Middle-East, and Africa — several of them clients of 20 years or more, some under NDA for their own designs. For brands and MNCs we make the full range as white-label, in your size, finish, and branding, with FITSTRUTS® as a ready stock option. For a complete size and weight chart or a white-label discussion, call +91-99888-54380 or email ashishint2001@gmail.com. Frequently Asked Questions Q1. What is a food grade stainless steel strut channel? A food grade stainless steel strut channel is a metal framing channel